If you’ve ever stood in a garage or a manufacturing plant, watching a radiator fin forming machine churning out those tiny, zig-zag metal fins like clockwork, you might’ve thought, “How the heck do these things get it so right every single time?” As a guy who’s spent the last 12 years building and fixing radiator fin forming machines, I’m here to break down the fin forming mold design principles that make that magic happen—no stuffy engineering jargon that’ll make your eyes cross. I’m not just a random writer; I’m a supplier, the kind of person you’d grab a coffee with (or a beer after a long day) to vent about production snags. I’ve seen what happens when a mold’s off by a hair—your fins don’t stack right, coolant doesn’t flow, and suddenly that new machine you bought is costing you more in downtime than it’s saving you. So let’s get into it, no corporate fluff. Radiator Fin Forming Machine
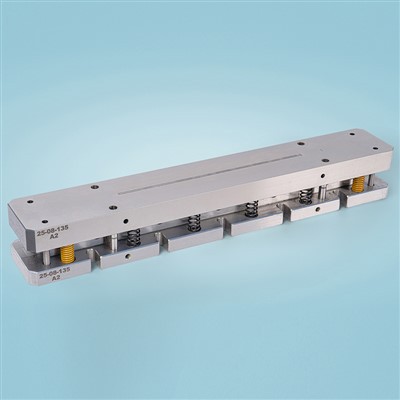
First off, let’s ground this: radiator fins aren’t just little metal bits. They’re the unsung heroes of heat transfer. A car’s radiator, an AC unit, a construction piece of equipment—they all rely on those thin fins to move heat from the coolant or refrigerant out into the air. If the fin’s shape is wrong, the whole system underperforms, overheats, or wastes energy. That’s why the mold that stamps those fins isn’t just a block of metal with a notch cut out. It’s the heart of the forming machine, and getting its design right separates the guys who sell you a machine that works from the ones who sell you a paperweight.
Let’s start with the number one rule I swear by: material compatibility. Wait, no—wait, let’s make it relatable. If you’re stamping aluminum fins (which 90% of radiators use these days because it’s light and cheap), your mold can’t be some off-the-shelf steel block from Home Depot. Aluminum’s soft, but it’s gummy—like overcooked taffy if it gets too hot when you’re forming it. If your mold’s made from regular carbon steel, it’ll wear out in 10,000 parts, max. I learned this the hard way 8 years ago when a shop I supplied bought a cheap mold online and burned through three in a month. Turns out, aluminum adhesion to carbon steel is a real thing—bits of aluminum would stick to the mold’s edges, warp the fin shape, and we’d have to stop the machine every 10 minutes to scrape it off. So we switched to tool steel with a chrome-plated or Teflon (wait, no, better—polished PVD coating) surface. PVD is Physical Vapor Deposition, for the nerds, but basically it’s a thin, slippery layer that doesn’t let aluminum stick. And if you’re working with copper? Different ballgame. Copper’s harder, so your mold needs more wear resistance—maybe D2 tool steel, heat-treated to 58 HRC (that’s hardness, don’t worry about the number, just know it’s tough). The big takeaway here: never use a one-size-fits-all mold. Match the mold material directly to the fin metal, or you’re gonna have so much downtime you’ll be throwing your hat at the wall during a shift change.
Next up: profile accuracy, and I mean down to the thousandth of an inch. Let’s talk about the fin’s cross-section—usually a zig-zag, or a serrated edge, or sometimes a louvered cut (those little slits that help air flow). The mold’s upper and lower dies (the two parts that do the stamping) have to be perfectly aligned, like a pair of scissors that doesn’t leave a bumpy edge. If there’s even a 0.001-inch gap between the dies, you’ll get “burrs” on the fins—sharp metal edges that can scratch the radiator tubes, clog the system, or even cause leaks. I once had a customer call me at 2 a.m. on a Saturday because their new machine was spitting out fins that had burrs so bad they were jamming the stacker. Turned out their mold manufacturer cut the dies 0.002 inches off center—easy fix, but it cost them $50k in lost production that weekend. How do we avoid that? We use CNC-machined dies with precision dowel pins that lock the upper and lower parts into place. No guesswork, no hand-filing (that’s a rookie move that leads to inconsistency). Also, the pitch of the fins—how far apart each zig-zag is—has to be consistent. If one fin’s 0.25 inches and the next is 0.24, when you stack them into the radiator core, there’ll be gaps where air doesn’t flow. The mold’s pitch lines have to be ground to the exact dimension, no shortcuts here. I tell all my customers: if your mold maker brags about “hand-finished dies,” run. CNC is non-negotiable for accuracy.
Then there’s formability, and this is where a lot of mold designers mess up—they get so caught up in the fin shape that they forget the metal has to bend without cracking or tearing. Aluminum, especially thin gauge (0.1 to 0.2 mm, usually), has a bend radius. That’s the smallest curve you can make in the metal without it breaking. If your mold’s bend radius is too tight, you’ll get cracks along the fin’s edge, which means heat transfer is garbage and the fin’s useless. We test this all the time: take a sample coil of aluminum, run it through a prototype mold, and check for cracks under a microscope (we don’t have fancy lab stuff, just a cheap $500 magnifier, works for us). Also, the way the metal flows through the mold is key. If the entry point is too sharp, the metal will snag, causing wrinkles. We add “lead-in ramps” to the first part of the die—gentle sloped edges that guide the thin metal into the forming section without tugging it. Think of it like driving up a curb vs. a ramp—you don’t scrape your tires on a ramp, same with metal. Another thing: springback. Metal doesn’t stay bent exactly how you form it; it “springs back” a little, like a paperclip bending back when you let go. For aluminum, that’s about 2-3% of the bend angle. So when we design the mold’s angle, we over-bend it by that 2-3% to account for springback. I’ve seen so many molds that looked perfect on the bench but made fins that were too straight once they came out—because the designer forgot about springback. That’s a rookie mistake, don’t let it be yours.
Coolant flow optimization, wait—no, that’s the fin shape, but the mold plays a part. Wait, no, let’s call it functional geometry. The mold isn’t just for stamping shape; it’s for making fins that do their job. Let’s talk about louvers—those little slits cut into the fin that lift air up and over, so it doesn’t just slip between the fins. If the louver angle is too steep, air gets turbulent and doesn’t flow; too shallow, and it does nothing. The mold’s louver punch has to be angled exactly, and the die has a matching pocket to cut that slit without tearing the metal. We do a lot of flow tests with our customers: we take a fin sample, put it in a wind tunnel (we rent a local lab’s, no need to buy one), and adjust the mold’s louver angle until we get the maximum air flow with the least pressure drop. It’s not set-it-and-forget-it. Every application—car radiator vs. forklift vs. home AC—needs a slightly different louver profile, which means a custom mold. I hate when suppliers say their mold works for everything—baloney. Heavy-duty equipment needs thicker fins, wider zig-zags, to handle vibration and heat. A tiny car radiator needs thinner fins, tighter louver spacing, for maximum heat in a small space. So don’t fall for the “one mold fits all” lie.
Wear resistance is another big one, because molds take a beating. They’re stamping thousands of parts a day, every day, so they have to hold up. We talked about material earlier, but there’s also surface treatment. For aluminum fins, we use chrome plating or that PVD coating I mentioned—both reduce friction between the mold and the metal, so less wear. For copper, maybe nitriding the die surface, which hardens it. The key here is that the wear doesn’t just happen on the flat parts of the die—it happens on the edges where you stamp the fins and louvers. If those edges get worn down, the fin’s profile starts to change. We recommend that our customers budget for mold maintenance every 6 months: take the dies off, send them out to be re-ground and re-coated. It’s way cheaper than buying a new mold every year. I had a customer who skipped maintenance and went two years—their mold got so worn that fins were 10% smaller than they should be, and they had to replace an entire batch of radiators for a client. That cost them $200k. Maintenance isn’t an extra expense; it’s an investment.
Wait, let’s talk about something that most mold design articles skip: ease of use. I’m a supplier, so I care about my customers not having to hire a team of engineers just to change a mold. A good fin forming mold should be quick to swap out—like, 15 minutes max, not an hour. So we design our molds with quick-lock clamps, not bolts that take forever to tighten. Also, alignment pins that don’t require special tools to line up. When you’re running a production shift, downtime for mold changes is money lost. I once visited a shop where their old mold took 45 minutes to swap, so they only changed molds once a day, even if they were switching between aluminum and copper. They lost 2 hours a day, every day, just on mold change time. That’s $10k a month in lost production, easy. So when we design our molds, we make sure they’re user-friendly, because even the best mold in the world is useless if your operators hate using it.
Let’s wrap this up with a real example to make it concrete. Last year, a small manufacturer of electric car radiators hit me up. They had an old machine, a cheap import, that was making fins with inconsistent louver angles, so their radiators were failing temperature tests. They were losing clients left and right. We designed a custom mold for them: used PVD-coated tool steel for aluminum, CNC-machined dies with 0.0005-inch alignment, over-bent for springback by 2.5%, quick-lock clamps for 10-minute swaps. They ran it for 8 months, no downtime from mold issues, their failure rate dropped from 12% to less than 1%, and they picked up three new automotive clients. They text me every now and then to say they still use that mold. That’s the kind of result we’re aiming for when we design these molds.
At the end of the day, fin forming mold design isn’t rocket science, but it’s not trivial either. It’s a balance between material science, precision machining, understanding how metal flows and springs back, and actually listening to what your customer needs (not just selling them a generic mold). I’ve been doing this for long enough that I can spot a bad mold design in 10 minutes of looking at a fin. It’s usually something small—too tight a bend radius, unaligned dies, no lead-in ramp—that causes big problems down the line.

If you’re in the market for a new radiator fin forming machine, or you’re sick of dealing with molds that wear out too fast, jam up, or just don’t get the job right, hit me up. I don’t do sales pitches that sound like a robot. I’ll ask you what kind of fins you’re making, what metal you’re using, how many parts you need per hour, and give you a straight answer on what mold design will work best for you. No fine print, no hidden fees, just actual advice from someone who’s built and fixed these machines for years. Let’s figure out what you need, so your production runs smooth and you can stop stressing about fin problems.
Stamping Die References
- Manufacturing Processes for Heat Exchangers, ASM International, 2019.
- Precision Die Design for Sheet Metal Forming, Society of Manufacturing Engineers, 2021.
- Aluminum Fin Forming Best Practices, International Heat Transfer Society, 2020.
Suichang Lvye Machinery Co., Ltd.
We are one of the most professional radiator fin forming machine manufacturers in China, also support customized service with low price. We warmly welcome you to buy discount radiator fin forming machine for sale here from our factory. If you have any enquiry about quotation, please feel free to email us.
Address: No. 402, Mudanting East Road, Miaogao Street, Suichang County, Lishui City, Zhejiang Province
E-mail: L528753@outlook.com
WebSite: https://www.suichanglvye.com/
